Choosing a supplier for flexible pvc injection molding requires more than comparing prices. The right partner must understand material behavior, mold design, production control, and your product’s daily use. A soft PVC part may look simple, yet small changes in hardness, wall thickness, or cooling time can affect sealing and durability.
Start by examining the supplier’s practical experience. Ask for relevant samples, process records, and clear explanations of their testing methods. A reliable manufacturer should discuss plasticizer selection, shrinkage control, flash prevention, and dimensional inspection without hiding behind vague promises. Look for quality systems, traceable batch records, trained technicians, and realistic production timelines. Their factory should also show clean work areas, organized tooling, and consistent inspection equipment.
Communication matters just as much. Request a detailed quotation that separates tooling, material, sampling, inspection, and shipping costs. Ask how design changes are handled after the first trial. A capable supplier welcomes technical questions and explains risks before production begins. No supplier is perfect. We may overlook a minor issue when a sample looks attractive. That mistake can become expensive after thousands of parts are produced.
This guide examines how to compare flexible pvc injection molding suppliers with greater confidence. It focuses on evidence, not polished sales language. You will learn how to assess technical capability, sample quality, capacity, communication, and long-term reliability. The goal is practical: select a partner that can repeatedly make safe, consistent, and functional PVC components for your application.
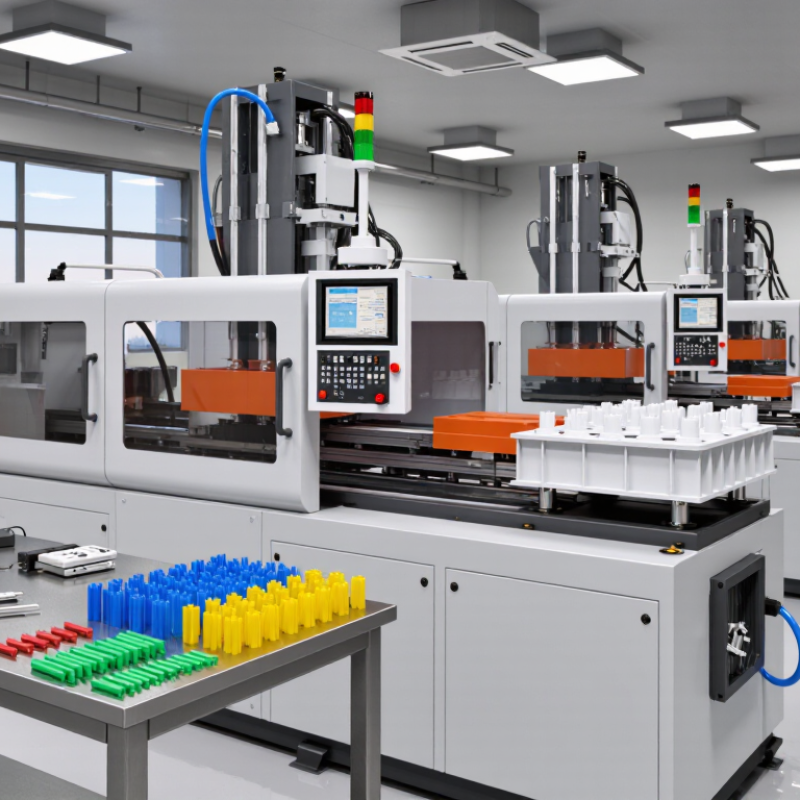
Define Your Flexible PVC Injection Molding Requirements
A reliable supplier starts with a precise part definition, not a sales quotation. Describe the product’s function, working temperature, chemical exposure, expected service life, and contact surfaces. Specify flexible PVC hardness in Shore A, wall thickness, draft angles, undercuts, color, texture, and dimensional tolerances. ASTM D2240 is commonly used for polymer hardness testing, while ISO 20457 addresses tolerances for molded plastic parts.
Your annual volume also changes the correct tooling decision. A 2024 market assessment by Grand View Research identifies automotive, construction, and healthcare as major demand areas for injection-molded plastics. These sectors often require tighter process control and stronger traceability. Ask suppliers how they control melt temperature, injection pressure, cooling time, and batch consistency. Request sample measurements, material certificates, and a documented validation plan. Small details matter. A soft seal may fail because of flash, shrinkage, or an unsuitable plasticizer.
Tips: Prepare a one-page requirement sheet before contacting suppliers. Include a 2D drawing, 3D model, target quantity, hardness range, tolerance table, and testing method. Discuss recycled content carefully, because it may affect odor, flexibility, and color stability. ISO 11469 can support polymer identification and marking practices. Do not accept “standard PVC” as a complete material specification. Define the formulation requirements.
A first draft is rarely right. Review the prototype after real assembly, not only on a workbench. That reflection can reveal excessive stiffness, difficult demolding, or a tolerance that serves no practical purpose.
Before evaluating suppliers, define the material hardness, required appearance, wall thickness, dimensional tolerance, production volume, and process window. The chart shows typical temperature ranges used as an initial reference for flexible PVC injection molding.
Typical starting ranges: barrel and nozzle temperatures are commonly controlled around 160–190°C, while mold temperatures are often maintained around 20–40°C. Final settings depend on the PVC formulation, part geometry, equipment, and quality requirements.
Choosing a flexible PVC injection molding supplier requires more than comparing quotations. Grand View Research valued the global PVC market at about USD 45 billion in 2023. Demand is growing, but material quality still varies widely. Ask for the PVC grade, plasticizer type, Shore A range, tensile data, elongation, and migration test results. Request a recent certificate of analysis for each production lot. Small differences matter.
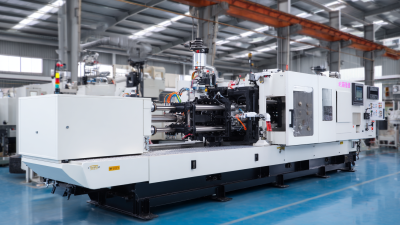
Inspect the equipment, not only the brochure. Flexible PVC needs controlled heating because excessive shear can cause discoloration and degradation. A capable supplier should show barrel temperature records, screw specifications, mold-flow experience, and preventive maintenance logs. Closed-loop pressure control can reduce flash and weight variation. ISO 20457 provides useful guidance for molded-part tolerances, although suppliers may interpret tolerances differently. Clarify them before tooling begins.
Production capability should be proven through a witnessed trial. Check cavity balance, cycle stability, automated feeding, in-process inspection, and batch traceability. Ask for capability data, such as Cpk, on critical dimensions and hardness. A supplier producing thousands of parts monthly may still struggle with a small, complex seal. That happened in one practical evaluation. The sample looked excellent, but its second-shift hardness drifted. Require pilot runs, retention samples, and documented corrective actions. Relying only on first-article approval is risky.
| Supplier Code | PVC Material Capability | Material Control and Traceability | Injection Equipment | Clamping Force and Part Size | Process Control | Quality Inspection | Production Capacity | Tooling and Engineering Support | Typical Lead Time | Overall Assessment |
|---|---|---|---|---|---|---|---|---|---|---|
| Supplier A | Flexible PVC compounds from approximately Shore A 50 to Shore A 90; capable of processing standard injection-molding grades and approved color concentrates. | Incoming-batch identification, supplier certificates, material drying records where required, and lot traceability through finished goods. | Hydraulic and servo-hydraulic injection machines with closed-loop temperature control and programmable injection speed. | Approximately 80–350 tonnes; suitable for small to medium-sized gaskets, seals, grips, caps, and protective components. | Recorded barrel temperatures, injection pressure, holding pressure, cooling time, and mold temperature for production jobs. | Dimensional inspection, visual inspection, hardness testing, weight checks, and sampling-based functional tests. | Approx. 150,000–300,000 small or medium parts per month, depending on cycle time and cavity count. | In-house mold maintenance and design-for-manufacturing review; limited capability for complex multi-material tooling. | 4–6 weeks after approved tooling and material confirmation | 4.4/5 |
| Supplier B | Flexible PVC generally covering Shore A 60 to Shore A 95, including grades formulated for abrasion resistance, weather resistance, and electrical insulation. | Batch certificates, first-in-first-out material handling, controlled storage, and documented color approval before mass production. | Servo-controlled machines with automatic feeding, process monitoring, and mold-temperature control for repeatable cycle conditions. | Approximately 120–500 tonnes; suitable for medium-sized technical parts and larger flexible molded components. | Statistical monitoring of key parameters, alarm limits for deviations, setup verification, and documented startup approval. | Dimensional reports, Shore hardness testing, tensile or elongation testing when specified, appearance inspection, and capability studies. | Approx. 300,000–700,000 small or medium parts per month, subject to tooling configuration and production schedule. | Strong mold-flow and DFM support, mold trials, cavity balancing, and corrective-action assistance during development. | 3–5 weeks for repeat products; 6–9 weeks for new tooling | 4.8/5 |
| Supplier C | Flexible PVC in a narrower range of approximately Shore A 70 to Shore A 90; best suited to standard non-medical industrial parts. | Basic purchase records and batch labeling are available; complete finished-part traceability depends on the project agreement. | Conventional hydraulic injection machines with standard temperature controllers and manual parameter verification. | Approximately 60–220 tonnes; suitable for simple, small molded parts with moderate dimensional requirements. | Operator-maintained process sheets and routine setup checks; limited automated data collection. | Visual inspection, basic dimensional checks, part-weight verification, and occasional hardness testing. | Approx. 80,000–180,000 small parts per month, depending on order mix and available machine time. | Basic mold fitting and maintenance; complex mold design and advanced engineering are usually outsourced. | 6–9 weeks, depending on tooling and production queue | 3.5/5 |
| Supplier D | Flexible PVC from approximately Shore A 45 to Shore A 85, including soft-touch and low-temperature flexible formulations subject to technical approval. | Full material-lot records, formulation approval procedures, retain samples, and documented change-control requirements. | Electric and servo-hydraulic injection equipment with precise metering, automated recipe control, and controlled material feeding. | Approximately 50–300 tonnes; optimized for small precision parts, overmolded components, and thin-wall flexible products. | Digital recipe management, first-article verification, real-time parameter monitoring, and documented process deviation handling. | Dimensional inspection, hardness, tensile and elongation testing, compression-set testing when applicable, and production part approval. | Approx. 200,000–500,000 small precision parts per month, depending on geometry, cavity count, and inspection requirements. | Advanced DFM support, insert and overmolding consultation, mold validation, and engineering change management. | 5–8 weeks for new projects; 2–4 weeks for repeat orders | 4.6/5 |
| Supplier E | Flexible PVC generally covering Shore A 65 to Shore A 95, with emphasis on cost-effective general-purpose molding grades. | Batch labels and incoming inspection are available; long-term traceability and retained samples are partially implemented. | Hydraulic injection machines with standard process controls and manually adjusted feeding and setup procedures. | Approximately 100–400 tonnes; suitable for medium-sized parts with relatively forgiving tolerance requirements. | Standard setup sheets and operator checks; limited capability for automated statistical process monitoring. | Visual inspection, basic dimensional inspection, weight checks, and periodic hardness verification. | Approx. 120,000–260,000 parts per month, depending on product size and production allocation. | Routine mold maintenance and basic tooling modifications; external support may be needed for complex designs. | 6–10 weeks, with longer schedules during peak production periods | 3.8/5 |
| Supplier F | Flexible PVC from approximately Shore A 50 to Shore A 90, with capability for flame-retardant, oil-resistant, and customized color formulations subject to validation. | Controlled material receiving, batch certificates, formulation records, retain samples, and traceability from raw material to shipping carton. | Servo-hydraulic machines ranging from small to large tonnage, with automated feeding, mold-temperature control, and production data collection. | Approximately 90–650 tonnes; suitable for small precision parts through larger flexible housings and protective components. | Documented process windows, parameter lockout, startup approval, capability monitoring, and corrective-action procedures. | Dimensional and visual inspection, hardness, tensile, elongation, compression-set, aging, and functional testing according to project specifications. | Approx. 400,000–900,000 parts per month across multiple production cells, depending on part complexity and cycle time. | Full tooling coordination, DFM review, mold-trial management, secondary-operation planning, and production ramp-up support. | 4–7 weeks for new programs; 2–4 weeks for established products | 4.7/5 |
| Supplier G | Flexible PVC in a general-purpose range of approximately Shore A 60 to Shore A 90; limited formulation development for specialized uses. | Material certificates and batch labels are available, but full process traceability should be confirmed before contract approval. | Mixed hydraulic and servo-hydraulic equipment with basic temperature control and limited automated monitoring. | Approximately 80–250 tonnes; appropriate for simple small and medium-sized components. | Standard work instructions and operator checks; parameter records are maintained primarily through production documents. | Visual inspection, sampling-based dimensional checks, and basic hardness testing when requested. | Approx. 70,000–160,000 parts per month, depending on order volume and machine availability. | Basic mold maintenance and production support; engineering assistance for complex parts is limited. | 7–10 weeks for new tooling and initial production | 3.2/5 |
When evaluating a flexible PVC injection molding supplier, inspect its quality system beyond attractive samples. A reliable supplier should control raw materials, mixing ratios, mold temperatures, injection pressure, and cooling time. Ask for documented inspection procedures and recent production records. Certificates alone are not enough. Paper is not proof.
Verify whether certifications match the facility, process, and intended application. Check certificate numbers, issuing organizations, expiration dates, and audit scope. For flexible PVC, request test data for hardness, tensile strength, elongation, compression set, and aging resistance. If relevant, confirm material compliance with applicable chemical and safety requirements. Lot traceability should connect each finished part to its compound batch and production date.
Product consistency becomes clearer during a factory visit or controlled trial order. Compare parts from different production runs, not just one approved sample. Measure dimensions at several points, inspect flash around the parting line, and check surface texture under consistent lighting. Samples can mislead. A supplier may perform well during development but struggle during volume production. I have learned that small variations in plasticizer content can change softness noticeably. Ask how deviations are handled, recorded, and corrected. A trustworthy team will explain weaknesses instead of hiding them. That honesty matters.
Choosing a flexible PVC injection molding supplier requires more than comparing the lowest quotation. Pricing should include tooling, material grades, color matching, inspection, packaging, and freight. A cheap quote may exclude essential services. Request an itemized proposal and confirm payment terms before approval.
Lead time should be measured from drawing approval to shipment. Ask for realistic dates for mold design, sampling, production, and final inspection. A reliable supplier explains capacity limits and identifies possible delays early. In practice, promised lead times can change when material availability shifts. That detail deserves written confirmation.
Communication and technical support often reveal a supplier’s real capability. During quotation, observe how clearly the team answers questions about shrinkage, wall thickness, flash, and part flexibility. Support should continue after sampling, especially when dimensions need adjustment. Delayed replies can create expensive production mistakes. I would not ignore that warning.
Tips: Ask for a sample timeline, inspection report, and escalation contact. Compare response times, not only prices. Request evidence of similar PVC projects, but protect confidential design data. Clarify whether engineering changes affect tooling costs or delivery dates. A short video call can expose unclear responsibilities quickly.
How to Choose a Flexible PVC Injection Molding Supplier?
Select the Supplier That Best Fits Your Project Needs
Your best supplier is not always the cheapest. Match the supplier to your part’s real demands. A 2024 PVC market analysis estimated global value at about US$45.7 billion in 2023. This growth increases supplier choices, but not every factory controls flexible materials well.
Ask for evidence, not promises. Review recent samples with similar wall thickness, hardness, and surface requirements. Check whether the supplier measures Shore hardness, shrinkage, flash, and dimensional stability for every production batch. The ISO 9001 quality framework can support consistency, but certification alone proves little. Audit the actual process. Watch material drying, mold temperature control, and first-piece inspection.
Project fit also includes communication. Confirm the supplier’s tooling experience, minimum order quantity, lead time, and change-control process. Request a material data sheet and traceability records for each PVC compound. Plastics Europe reported approximately 54.1 million tonnes of plastics production in Europe during 2023. That figure shows the scale of the industry, not guaranteed quality. Bigger capacity may still mean slower attention.
A practical trial helps. Send a small pilot order and measure parts after cooling, not immediately after molding. Discuss failures openly. I would not trust a supplier that claims zero defects without showing inspection records. That sounds impressive, but real production needs controlled responses. Choose the team that understands your application, documents its decisions, and improves when the first result is imperfect.