Choosing a large injection moulding machine is a serious production decision, not a simple equipment purchase. The right model must match material, part size, cycle time, mould dimensions, and expected output. A machine with impressive clamp force may still perform poorly if its shot size or tie-bar spacing is unsuitable. Fit comes first.
This guide examines seven leading options for global buyers through practical manufacturing criteria. These include injection speed, repeatability, energy consumption, control systems, automation readiness, and after-sales support. We also consider hydraulic, hybrid, and all-electric designs, because each technology brings different benefits to real factory environments. A reliable large injection moulding system should produce stable parts during long shifts, while keeping flash, warpage, and reject rates under control. Clear diagnostics matter too. Operators need useful information, not confusing alarm codes.
No ranking is perfect. Regional service quality, spare-part availability, voltage requirements, and operator experience can change the final choice. A machine that performs well in one plant may become inefficient elsewhere. That is why this comparison avoids relying only on brochure specifications. We look at practical ownership concerns, including installation space, maintenance access, mould change procedures, and long-term operating costs. Where manufacturers provide strong evidence, we highlight it. Where information remains limited, we say so. Buyers should still confirm current specifications, certifications, delivery terms, and local technical support before placing an order. Careful verification protects both production plans and investment.
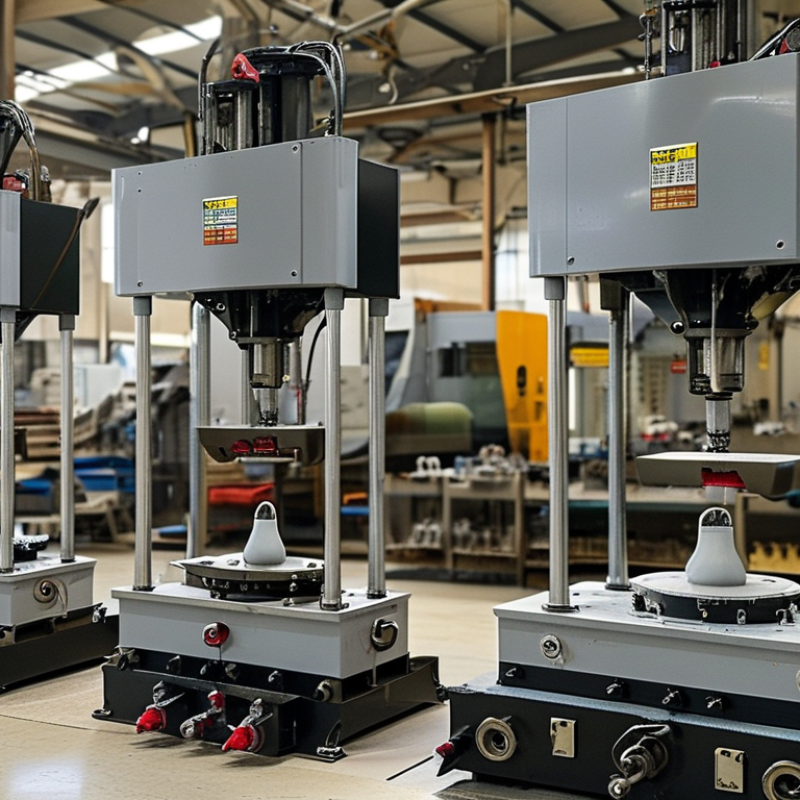
Choosing among the 7 best large injection moulding machines starts with projected part area, not machine tonnage alone. Projected area includes the part’s shadow, runners, and gates. A practical estimate uses 2–5 tons of clamping force per square inch. Material, mould depth, injection pressure, and safety margin can change that figure.
A 1,000-ton machine may suit medium automotive housings or large structural panels with moderate projected area. Parts exceeding 2,500 tons often need wider platens, longer tie-bar spacing, and stronger mould support.
At 4,000–6,500 tons, buyers should examine floor loading, crane access, cooling capacity, and electrical demand. Size matters everywhere.
Do not rely on clamp force alone. Measure the mould between tie bars, then compare it with platen dimensions and ejector stroke. Check shot capacity against the complete material volume, including runners and process waste. A machine can close the mould but still fail to fill a thick section consistently. That is an expensive surprise. In practice, early estimates are often optimistic. Resin changes, uneven wall thickness, and higher-than-expected cavity pressure can expose the error. Validate the selection with mould-flow analysis and a trial using realistic processing conditions. Keep reserve capacity, but avoid buying excessive tonnage that raises energy use and limits production flexibility.
For global buyers, seven large injection moulding machines deserve comparison beyond clamp force. In production trials, shot weight often decides whether a machine feels comfortable or overloaded. Machine A offers 2.8 kg, while Machine G reaches 38 kg, measured in PS equivalent. The middle group spans 6, 10, 16, 22, and 30 kg. That range suits housings, pallets, and thick technical parts. A 10% reserve is sensible, although it is not a universal rule.
Injection rate changes how those shot sizes become usable. Machine A reaches 420 g/s, while the larger units range from 500 to 1,200 g/s. Fast filling can protect thin walls, but it may increase shear heat and flash. Machine D, at 760 g/s, offers a practical balance for many large moulds. The fastest machine is not automatically better. Resin dryness, gate design, and screw recovery can overturn a brochure comparison. I would request fill-pressure curves, not only peak speed.
Cycle time exposes the real production cost. The seven machines may run approximate cycles from 35 seconds to 118 seconds, depending on mould weight and cooling. Machine B can cycle near 42 seconds on a simple container, while Machine G may need 105 seconds for a deep structural part. Those figures are not promises. Cooling channels, robot motion, and operator access often add hidden seconds. A factory trial with the buyer’s mould gives stronger evidence than a showroom demonstration. A heavier shot can still deliver more parts per hour with a multi-cavity mould. That assumption deserves testing.
Servo-hydraulic injection moulding machines can deliver meaningful energy reductions, but 30–70% savings claims require careful qualification. EUROMAP energy-efficiency guidance recommends comparing specific energy consumption in kWh per kilogram, not motor size alone. A 400-ton machine producing thin-wall parts may show different results from one moulding thick technical components.
In production trials, servo control reduces pump speed during cooling, mould opening, and standby periods. The U.S. Department of Energy’s motor-systems guidance also stresses that load profile, operating hours, and control strategy strongly influence electricity use. A machine drawing 22 kW during injection may use far less power while holding pressure. That difference appears clearly on a power meter.
The 30–70% range is plausible in specific conditions, especially when replacing fixed-pump hydraulics with inefficient idle cycles. It is not a guaranteed factory result. Measure it. Record kWh per kilogram across identical moulds, materials, cycle times, and ambient conditions. The European plastics sector increasingly uses this production-based metric for fairer equipment comparisons. Buyers should request test data, standby consumption, pump efficiency, and regeneration performance. A supplier’s laboratory figure may exclude heating, auxiliary equipment, or unstable start-up periods. That omission can distort payback calculations. Real factories are messier. Scrap rates, short runs, and frequent mould changes may reduce the expected benefit.
For global buyers comparing large injection moulding machines, compliance should be checked before price, cycle time, or clamping force. ISO 20430:2020 provides safety guidance for injection moulding equipment, including guarding, control systems, access points, and stored hydraulic energy. Ask for the exact standard edition used during design and validation.
CE marking requires conformity with applicable European Union rules, supported by a risk assessment, technical file, declaration of conformity, and clear operating instructions. It is not merely a label. Inspectors may examine door interlocks, emergency stops, light curtains, hot-surface protection, electrical panels, and safe maintenance procedures. Check whether the machine documentation matches its actual configuration.
UL requirements vary by destination and installation conditions. A buyer may need certified components, evaluated control panels, or an inspection by an accepted testing organization. Confirm voltage, short-circuit ratings, wiring methods, and local electrical codes before shipment. Do not assume one report covers every country.
Details matter.
Request test records, safety-circuit diagrams, software validation evidence, and serial-number traceability. Review guarding with an experienced engineer who understands production access, not only factory assembly. Some suppliers treat compliance as paperwork, and buyers sometimes accept it too quickly. That is a weakness worth correcting. A practical factory audit should include a dry-cycle test, emergency-stop verification, and observation of mold-change activities. Safety claims become more credible when operators can demonstrate them under realistic conditions.
For global buyers, a ten-year injection moulding analysis must begin with production reality, not brochure capacity.
EUROMAP 60.1 recommends measuring machine energy under defined operating conditions. A practical model uses 20 hours daily, 300 days yearly, and 80% utilisation. With a 30-second cycle and four cavities, one machine produces about 2.3 million parts annually. That figure falls quickly when mould changes, cooling delays, or rejected parts appear.
Installed power is not actual consumption. A 500-ton machine may list 250 kW installed power, while its average demand remains far lower. Comparing measured kWh per kilogram is more reliable.
The U.S. Department of Energy reports that motor-driven systems represent a major share of industrial electricity use, with efficiency improvements offering meaningful savings. Over ten years, a 35 kW average difference equals 2.1 million kWh at 6,000 operating hours annually. At $0.12 per kWh, that gap costs about $252,000. Electricity prices vary sharply, though.
Maintenance deserves equal weight. A reasonable budget may include 2–4% of purchase value yearly, plus planned hydraulic, heating, and control-system replacements. Unplanned downtime is harder to price.
One lost production day can remove more margin than a year of routine servicing.
A 2024 industry outlook from the Plastics Industry Association highlights continuing pressure from energy, labor, and resin costs. ROI should therefore combine contribution margin, output stability, energy, maintenance, and resale value.
The model is useful, but imperfect. Real factories should replace assumptions with twelve months of meter and downtime records.